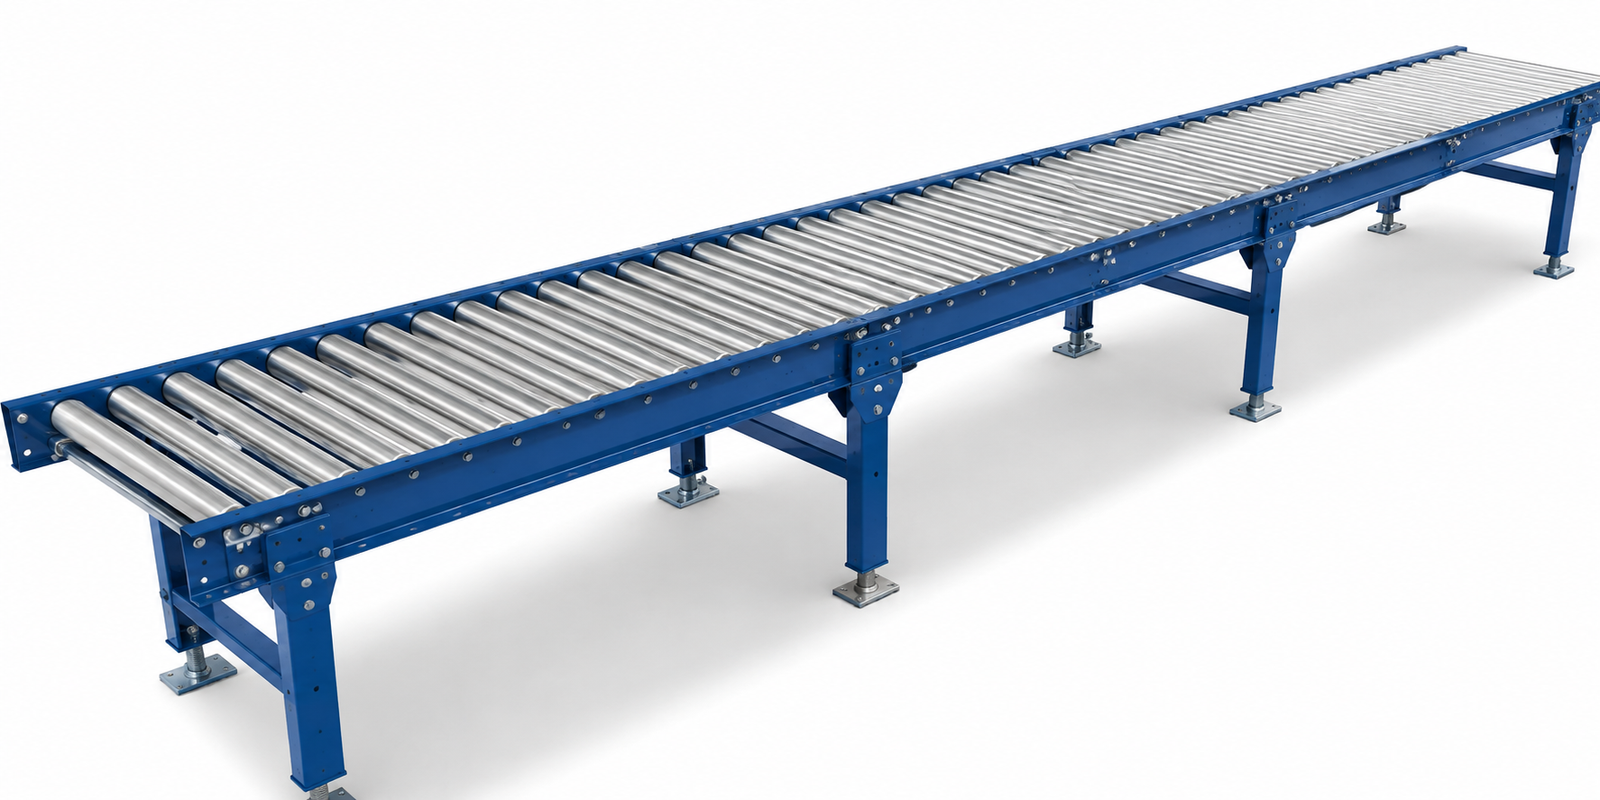
Flat Belt Conveyor systems are widely suitable for food and consumer goods industries because they provide a simple and efficient way to move products through different stages of production, processing, packaging, and dispatch. These industries often handle a large volume of products that need to move continuously while maintaining an organized workflow.
From packaged food items and containers to consumer products and cartons, efficient material handling plays an important role in maintaining production speed. A properly selected flat belt conveyor can help businesses reduce unnecessary manual movement and create a smoother flow between different operational areas.
Supporting Smooth Product Movement
Food and consumer goods facilities often involve multiple stages before products are ready for distribution. Materials may move through processing, inspection, packaging, labelling, and dispatch.
Manual transportation between these stages can slow down operations, particularly when production volumes are high. A Flat Belt Conveyor creates a dedicated route for moving suitable products from one workstation to another.
The continuous conveying surface helps maintain a steady product flow and reduces unnecessary delays between connected processes.
Suitable for Different Product Types
Food and consumer goods industries handle products in a variety of shapes, sizes, and packaging formats. A flat conveyor surface can be suitable for transporting items such as:
- Packaged food products
- Cartons and boxes
- Bottles and containers
- Consumer goods
- Pouches and packets
- Components and packaged materials
The conveyor should be selected based on product weight, dimensions, surface characteristics, production capacity, and operating requirements.
A properly designed system helps ensure that products move efficiently without creating unnecessary handling challenges.
Reducing Manual Material Handling
Repeated manual transportation can require significant time and workforce involvement. Employees may need to carry products between different machines or workstations throughout the day.
A Flat Belt Conveyor helps automate this movement by providing a continuous transportation path. Products can move between designated points with reduced manual intervention.
This allows employees to focus on other important activities, including product inspection, quality control, packaging, labelling, and equipment monitoring.
Reducing repetitive handling can also help businesses create a more organized production environment.
Supporting Efficient Packaging Operations
Packaging is an important stage in both food and consumer goods manufacturing. Products often need to move quickly between filling, sealing, labelling, inspection, and packing stations.
A flat belt conveyor can connect these stages and help maintain a consistent supply of products to each workstation. When the conveyor speed is properly matched to production requirements, it can reduce unnecessary waiting time and help prevent product accumulation.
This supports a more coordinated packaging process and improves overall workflow efficiency.
Helping Maintain an Organized Production Flow
Efficient production depends on knowing where materials are moving and how different stages are connected. Without a structured material handling route, products may be placed temporarily on floors, tables, or storage areas while waiting for the next process.
A Flat Belt Conveyor provides a defined transportation route. This can help businesses maintain better organization and make it easier to monitor product movement.
A structured workflow can also help managers identify potential bottlenecks and improve coordination between different departments.
Supporting Automation in Consumer Goods Industries
Many food and consumer goods manufacturers are increasing their use of automation to manage growing production volumes. Conveyor systems can provide an important connection between automated and manual processes.
A flat belt conveyor can transport products between processing equipment, packaging machinery, inspection stations, and dispatch areas. This reduces the need for repeated manual transfers and supports a more integrated production line.
Businesses can also plan conveyor systems with future expansion requirements in mind.
Importance of Reliable Conveyor Solutions
Working with experienced Conveyor System Manufacturers in India can help businesses select material handling solutions based on their specific operational requirements. Factors such as production volume, product characteristics, available space, conveyor speed, and integration needs should be considered before selecting a system.
Reliable conveyor design and proper installation can support consistent performance and long-term operational efficiency.
Businesses looking for industrial material handling solutions can explore Tech Trek Engineering for different conveyor applications designed to support manufacturing and processing operations.
For businesses specifically looking to improve product transportation, Tech Trek Engineering’s Flat Belt Conveyor can be explored for suitable industrial material handling requirements.
Making Better Use of Available Space
Production facilities often need to accommodate machinery, storage areas, employee workstations, and transportation routes within limited space.
A properly planned conveyor layout can help create a more organized facility. Instead of employees repeatedly transporting products across the production floor, the conveyor establishes a dedicated path for material movement.
This can improve workflow organization and allow businesses to make better use of available operational space.
Supporting Long-Term Productivity
A conveyor system can provide benefits beyond faster product transportation. By reducing repetitive manual movement and connecting different stages of production, businesses can improve overall workflow consistency.
As production requirements increase, a suitably designed conveyor system can also support higher material volumes and future automation goals.
Regular maintenance is important for maintaining reliable performance. Belts, rollers, bearings, drive components, and supporting structures should be inspected periodically to identify potential issues early.
Conclusion
Flat Belt Conveyor systems are suitable for food and consumer goods industries because they support smooth product movement, reduce repetitive manual handling, improve packaging workflows, and help create more organized production operations.
By selecting a conveyor according to product characteristics and facility requirements, businesses can improve material flow and support long-term productivity. Working with reliable Conveyor System Manufacturers in India can also help ensure that the selected system meets current operational needs while supporting future growth.
Frequently Asked Questions
1. What is a Flat Belt Conveyor used for?
A Flat Belt Conveyor is used to transport products and materials between different stages of manufacturing, processing, packaging, and dispatch operations.
2. Why is a Flat Belt Conveyor suitable for food and consumer goods?
It provides a smooth and continuous surface for transporting suitable packaged products, containers, cartons, and consumer goods through production and packaging areas.
3. Can a Flat Belt Conveyor support automated production lines?
Yes. It can connect different machines and workstations, helping products move between processing, inspection, packaging, and dispatch stages with reduced manual handling.
4. How does a Flat Belt Conveyor reduce manual work?
It automates the transportation of products between designated points, reducing the need for employees to repeatedly carry materials across the facility.
5. What should businesses consider before choosing a conveyor?
Important factors include product size, weight, required capacity, conveyor speed, facility layout, available space, and integration with existing equipment.
6. How can Conveyor System Manufacturers in India help businesses?
Conveyor System Manufacturers in India can help businesses evaluate their material handling requirements and select suitable conveyor configurations for efficient and reliable operations.