Bucket Elevator Manufacturer
- Home
- Bucket Elevator
Custom Heavy-Duty Bucket Elevator Systems
Moving thousands of tons of bulk materials vertically day after day isn’t easy. If you’re comparing designs, discharge styles, and belt versus chain drives, feeling overwhelmed by technical options is completely normal. Choosing the wrong setup risks costly floor bottlenecks, material degradation, or frequent operational downtime. At Tech Trek Engineering, we design and manufacture custom bucket elevators built for long service life, minimal upkeep, and zero material loss. Whether you’re handling fine powders, heavy minerals, or delicate agricultural products, this guide walks you through every detail so you can select the right elevator system with complete confidence.
What Is a Bucket Elevator?
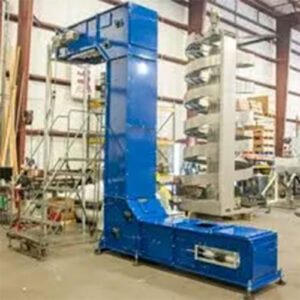
A bucket elevator is a continuous vertical material handling conveyor engineered to lift bulk dry materials, powders, aggregates, or granular solids straight up through enclosed, dust-tight casings.
Core Components
-
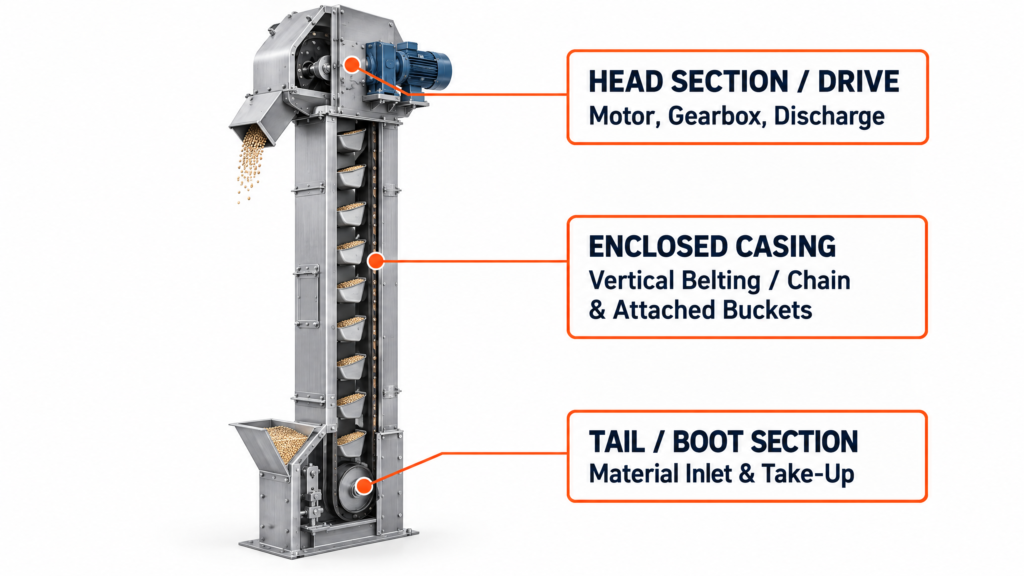
Head Section: Positioned at the top, housing the main drive motor, drive pulley or sprocket, discharge chute, and backstop device to prevent reversing.
-
Casing / Trunking: Heavy-gauge sheet steel enclosures that contain dust, protect internal components from weather, and keep work areas safe.
-
Traction Medium: A durable elevator belt (rubber/fabric or steel cord) or high-tensile steel chain running continuously between top and bottom pulleys.
-
Buckets: Available in ductile iron, fabricated steel, nylon, or polyethylene, sized specifically for your bulk material density.
-
Tail Section (Boot): The bottom loading zone featuring an internal boot pulley, inlet hopper, and manual or automatic screw take-up units to maintain proper line tension.
How Bucket Elevators Work
Material enters through the lower inlet hopper directly into the boot section. As the continuous belt or chain moves upward, the attached buckets scoop or collect the material, carry it vertically through the dust-tight casing, and invert over the top head pulley to discharge into storage silos, hoppers, or downstream process equipment such as screw conveyors or pneumatic conveying systems.
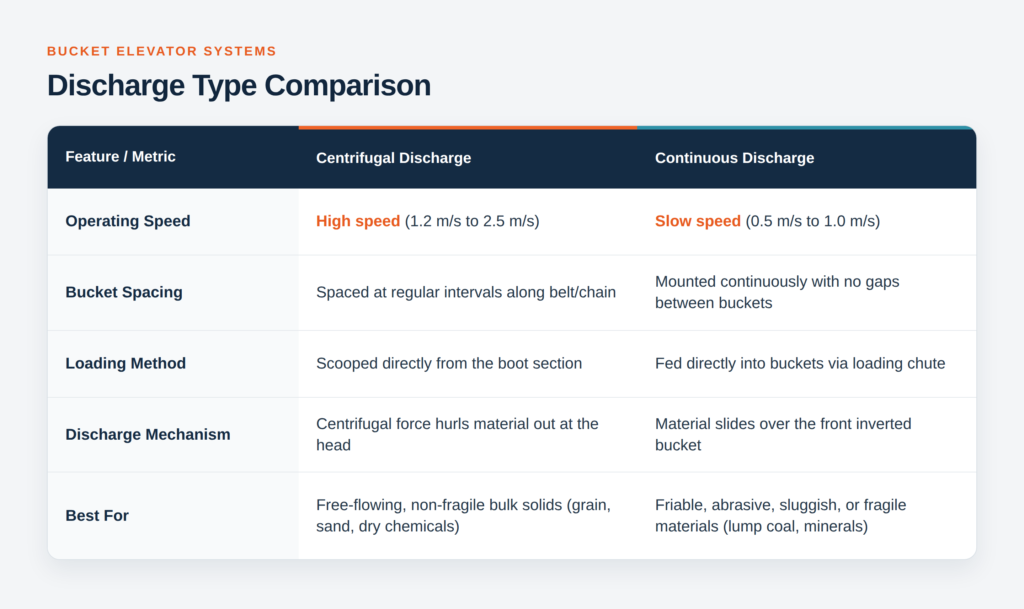
Continuous vs. Centrifugal Discharge Elevators
Selecting the correct discharge mechanism is the single most critical decision when configuring your bucket elevator. Using the wrong speed or bucket spacing causes material backlegging (material falling back down the casing) or severe product damage.
Key Types of Bucket Elevator Systems
1. Belt Bucket Elevators
-
Best suited for: High-speed vertical lifting of non-abrasive to moderately abrasive materials like grain, seeds, fertilizer, and light chemicals.
-
Advantages: Quiet operation, lightweight, lower initial cost, and smooth running at elevated speeds. Need horizontal transfer as well? Explore our belt conveyor systems.
2. Chain Bucket Elevators (Single & Double Strand)
-
Best suited for: Heavy-duty, high-temperature, or ultra-abrasive bulk materials like clinker, cement, aggregates, and heavy ores.
-
Advantages: Exceptional tensile strength, heat resistance up to $250^\circ\text{C}+$, and positive sprocket drive engagement under heavy loading. They pair well with our chain conveyors in heavy-duty lines.
3. Positive Discharge Elevators
-
Best suited for: Sticky, light, or sluggish materials that cling to bucket walls.
-
Advantages: Auxiliary sprockets physically tilt the buckets completely upside down over the discharge chute for thorough emptying.
How to Choose the Right Bucket Elevator for Your Facility
When requested by our engineering team, having these four key parameters ready helps us size and configure your unit accurately:
-
Material Characteristics: Bulk density ($\text{kg/m}^3$), moisture content, particle size distribution, abrasiveness, and temperature.
-
Required Throughput Capacity: Desired volumetric or mass flow rate (expressed in tons per hour, or $\text{TPH}$).
-
Discharge Height: Total vertical lift required from the boot inlet flange to the top discharge centerline.
-
Operating Environment: Indoor, outdoor exposed, explosive environments (requiring ATEX / dust explosion vents), or sanitary food/pharma standards.
Why Work with Tech Trek Engineering?
-
Tailor-Made Configurations: We custom-engineer bucket heights, casing thicknesses, drive sizes, and bucket profiles to fit your exact footprint—no off-the-shelf compromises.
-
Heavy-Duty Construction: Built using reinforced steel casings, wear-resistant head liners, and premium sealed bearings for maximum operational uptime. See our tips on ways to reduce conveyor maintenance cost.
-
Dust & Safety Compliant: Fully enclosed casing joints, integrated explosion relief panels, inspection access doors, and zero-speed switches keep your plant safe and clean.
-
Full Application Support: Our team assists you through initial material sizing, technical layout drawings, and post-installation technical support. See examples of our work in the gallery.
Frequently Asked Questions
What is the difference between a bucket elevator and an inclined belt conveyor?
A bucket elevator transports material vertically (up to 90° angles) within a compact footprint, making it ideal for tight plant layouts. See why bucket elevators outperform vertical conveyors for bulk handling. Inclined belt conveyors require significantly more floor space due to incline angle limitations (typically maximum 18° to 22°).
How do I prevent material from falling back down the casing (backlegging)?
Backlegging occurs when operating speeds are miscalibrated or when bucket design does not match the material’s discharge path. Correct head pulley sizing, proper bucket geometry, precise speed control, and correct chute positioning eliminate backlegging completely. For other causes, see our guide to common bucket elevator operational problems.
How often do elevator belts or chains require maintenance?
Routine maintenance involves checking belt/chain tension weekly, inspecting bucket attachment hardware monthly, and monitoring bearing lubrication every 500 operating hours. Integrated automatic take-up units help maintain steady tension automatically. Plants can also adopt predictive conveyor maintenance to catch tension and bearing issues early.
Learn more in our guide: why industries trust a reliable bucket conveyor manufacturer for vertical material transport.
Related bulk handling solutions: screw conveyors for heavy-duty material handling, drag chain conveyors for bulk material handling, and trough conveyor systems. Or browse all our conveyor products.