Why Businesses Trust a Wire Mesh Belt Conveyor for Reliable Performance
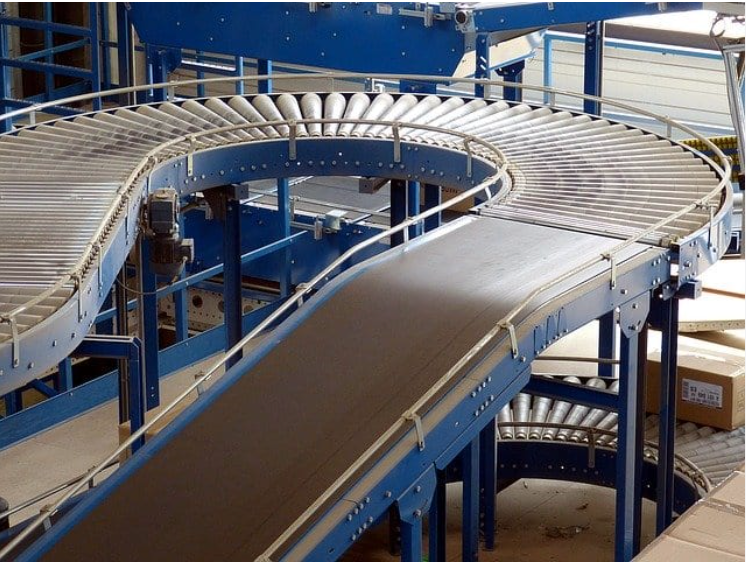
Wire mesh belt conveyor systems are widely used by businesses that require dependable material handling, controlled product movement, and reliable performance across demanding industrial processes. Their open mesh construction makes them particularly useful for applications involving heating, cooling, drying, washing, baking, coating, and other processes where airflow or liquid drainage is important. From food processing […]